Case studies
Measurable outcomes, repeatable patterns
Examples of digitization, ERP–shopfloor integration, error-proofing, and inventory systems with clear results.
Spare Parts Store Digitisation
Industrial manufacturing•
Problem
Manual packing and dispatch verification caused delays, data inconsistencies, and compliance risk at high throughput.
Solution implemented
SCMOPSAIDCCompliance labeling
Results
Faster GRR → dispatch movement
Lower manual verification effort
Before vs After
- Paper/manual checks at packing
- Delayed ERP updates
- Limited traceability on shipment units
- Scan-verified packing workflow
- Real-time ERP interfacing
- QR traceability + compliant labels
Compliance workflowERP interfaceQR traceability
Assembly Line Digitisation
Assembly operations•
Problem
Spreadsheet-based reporting hid downtime drivers and slowed corrective actions across shifts.
Solution implemented
MFGOPSERP integrationIoT/PLC data capture
Results
Recovered production capacity
Before vs After
- Manual downtime logs
- Delayed KPI visibility
- Inconsistent production data
- Real-time downtime capture
- Automated ERP transactions
- Shift-ready dashboards and alerts
Downtime captureQuality monitoringERP automation
Lean Inventory Management & JIT
Supply chain•
Problem
Excess line-side stock increased handling, space usage, and planning noise, without improving output stability.
Solution implemented
SCMOPSJIT workflowsInventory visibility
Results
Replenishment predictability
Before vs After
- Overstocked line-side areas
- Reactive replenishment
- Low visibility on consumption signals
- Consumption-driven controls
- JIT replenishment loops
- Real-time inventory dashboards
Consumption-drivenJIT replenishmentInventory turns
Kitting, Sequencing & Poka‑Yoke
Line-side feeding•
Problem
Incorrect kits and sequence breaks caused frequent line stops, rework, and high dependence on supervision.
Solution implemented
SCMOPSPoka‑Yoke SystemsPick‑to‑Light
Before vs After
- Manual kit checks
- Frequent sequence breaks
- High supervision dependency
- Error-proof kitting validation
- Sequence-controlled feeding
- Predictable line-side execution
Error proofingTakt stabilityLower supervision
Maruti Suzuki Robotic Platform & Layout Engineering
Automotive body welding•Maruti Suzuki
Problem
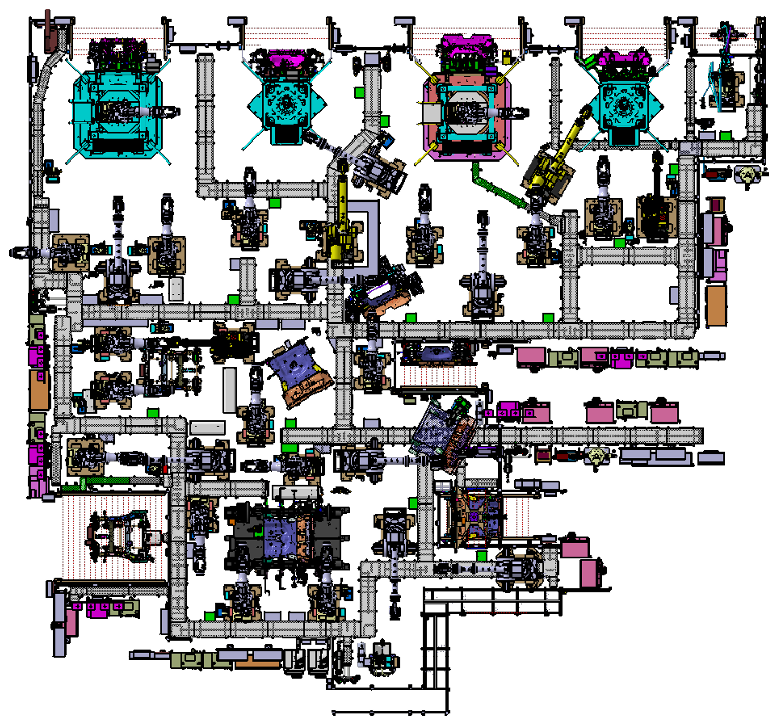
The program required precise robotic platform and layout engineering to support a dense automation setup with reliable manufacturability.
Solution implemented
Process & Layout DesignMechanical DesignRobotic Simulation/Process Simulation2D Detailing
Results
Robots covered in full layout scope
Detailed layout footprint
Platform engineering scope
Before vs After
- Distributed design inputs across automation and layout teams
- Higher coordination load for release-quality 2D/3D outputs
- Risk of delays in implementation-ready documentation
- Integrated layout + platform engineering package
- Structured 3D and 2D detailing for release readiness
- Cleaner handoff to manufacturing and site execution teams
YAAN EngineeringRobotic layout2D + 3D detailing
Wooshin Welding Fixture Engineering Program
Automotive fixtures and tooling•Wooshin India Pvt. Ltd.
Problem
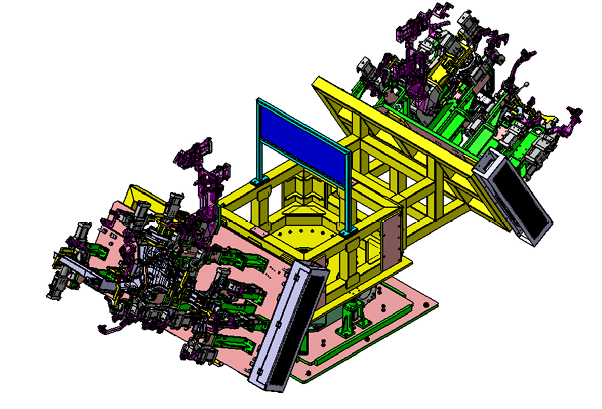
Multiple body-line fixture programs needed high-quality design and detailing output within delivery windows while maintaining tooling robustness.
Solution implemented
Tool DesignMechanical Design & 2D DetailingProcess DevelopmentProject Management
Results
Major fixture programs executed
Long member line coverage
Design-to-release support delivered
Before vs After
- Complex fixture requirements across different line programs
- High dependency on synchronized design and release workflows
- Tight delivery windows for manufacturing support
- Program-specific fixture concepts and detailed releases
- Improved alignment between tooling design and fabrication
- Streamlined documentation package for execution
YAAN EngineeringWelding fixturesTool design
Want a similar outcome?
Share your current process and constraints. We’ll propose a phased plan with feasibility, ROI estimation, and a rollout strategy built for adoption.